Precision TIG Welding for High-Quality Joints

Understanding TIG Welding: A Comprehensive Overview
TIG welding, short for Tungsten Inert Gas Welding, is a highly versatile method used for joining metals. Unlike spot welding, which creates weld scars with a single click on the workpiece, TIG welding involves the use of a tungsten electrode to create an electric arc, which melts the base metal and filler material (if used) to form a weld bead.
This welding technique is particularly well-suited for welding high-purity materials and special alloy materials. It finds extensive application in the manufacturing and processing of stainless steel, where its precision and control are highly valued. Whether it’s manual welding or automatic welding of stainless steel ranging from 0.5mm to 4.0mm thick, TIG welding remains the preferred method.
TIG Welding Process in Action
In applications such as bottom welding of pressure vessels, TIG welding with filler wire is commonly employed. This is due to the superior air tightness and reduced porosity achieved by TIG welding, making it ideal for critical applications. However, it’s important to note that TIG welding generates significant heat, necessitating post-weld polishing to remove any scars or imperfections. Therefore, the skills and experience of welders play a crucial role in ensuring the quality of TIG welds.
Advantages and Disadvantages of TIG Welding in Sheet Metal Fabrication
TIG welding is widely used in metal fabrication. It can be applied to both flat metal sheets and irregular‑shaped workpieces. When there is a large gap between metal sheets, filler rod can be used as filling material to join the two pieces. Spot tack welding may be performed first for positioning, followed by fully welding. Overall, TIG welding offers excellent controllability and versatility, making it a preferred choice for various welding applications, especially those requiring precision and high-quality welds. Despite its widespread use, there are two key points regarding TIG welding that require special attention:
1. Lack of fusion
Insufficient heat input fails to melt the base metal at the joint. The filler rod only sits on the surface without metallurgical bonding. The weld is prone to cracking under load.
2. Burn-through
Excessive heat input melts a hole through thin sheet metal. It commonly occurs on 0.3–1.5mm thin plates. Although TIG welding enables precise heat control, thin sheet welding is technically demanding.
Therefore, achieving a high-quality weld requires not only the right equipment but also extensive hands-on experience. At NEMEZ Metalworks, our management team and skilled welders each bring more than 18 years of experience in metal fabrication. This deep expertise allows us to maintain strict control over every stage of the welding process, from fit-up and positioning to final welding, ensuring consistent quality and reliable results.
TIG Welding: Finished Results


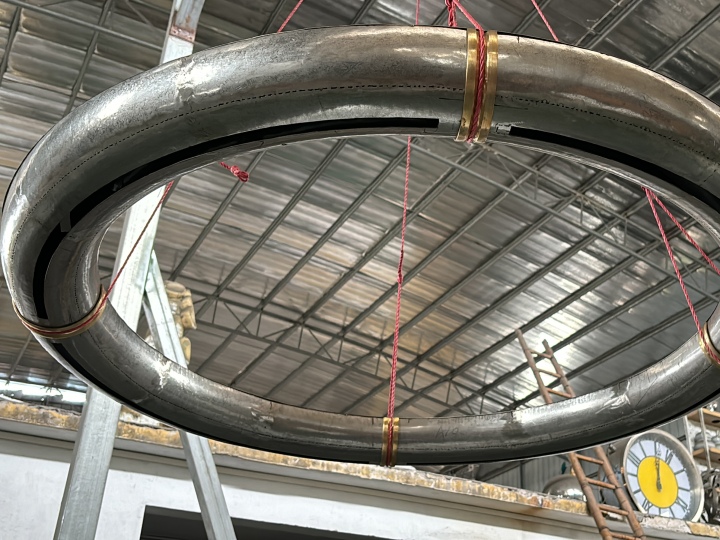
TIG welding leaves heat tint on stainless steel welds. Pickling & passivation or grinding/polishing can restore corrosion resistance. Dark blue or black oxidized areas tend to rust if left untreated.
As shown in both the video above and the images, our welders carefully work on the TIG-welded areas by lightly tapping and removing excess filler material before proceeding with the full weld. After the parts are properly positioned and tack-welded, the joints are fully welded, followed by a final grinding process to smooth and refine the welds.
FAQ About TIG Welding:
Both TIG welding and laser welding are widely used in metal fabrication, but they differ in how they handle gaps and joint shapes. When there is a larger gap between two metal sheets, TIG welding can use welding wire as a filler material to bridge the gap and join the two pieces together. The parts can first be tack welded for positioning and then fully welded to complete the joint. TIG welding can be used for both flat metal sheets and irregularly shaped metal components, while laser welding generally requires the two metal pieces to fit together with very little gap between them. For irregularly shaped metal components, laser welding can be more limited because the joint may not be close enough for the laser to achieve a proper weld.
As mentioned above, the TIG welding process can use filler material (welding wire), which uses high temperature to melt the base material and welding wire at the joint, and the molten metal mixes and fuses together after cooling.


